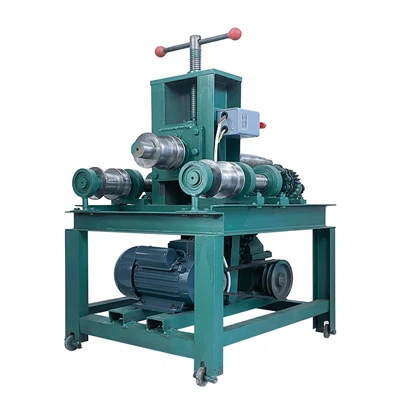
If you work in metal fabrication, you’ve probably noticed that a cold roll forming machine can feel like the backbone of your operation—until it doesn’t keep up with tighter tolerances, faster runs, or new product lines. As a cold roll forming machine supplier, I’ve helped dozens of fabricators upgrade their equipment over the last 12 years, and I’ll tell you this: upgrading isn’t just about swapping out a single part. It’s about aligning every component with your current and future production goals, without the downtime that can derail your bottom line. Cold Roll Forming Machine

Let me start with a common mistake I see first-time upgrade seekers make: they jump straight to buying a new roll set or a control panel without mapping out what their facility actually needs. Last year, a customer in Pennsylvania reached out because his old machine could only form 12-gauge steel, and he wanted to add 14-gauge aluminum parts for a new trailer project. He’d already priced a $15,000 roll set upgrade, but after a 45-minute on-site assessment, we realized his motor and gearbox were only rated for 12-gauge—adding 14-gauge would lead to premature wear, or worse, a breakdown mid-run. We adjusted his plan: a 5-horsepower motor upgrade and a revised roll set, which cost 30% less than his original plan and got him up and running in three days instead of one. That’s why the first step of any upgrade is a thorough, facility-specific audit—not a one-size-fits-all quote.
The audit should cover three core areas: your current production output, your target parts, and your maintenance history. Let’s break that down. First, production output: how often are you running overtime, or slowing down to avoid jams? If your machine is operating at 70% of its rated speed because of frequent shear breaks or alignment issues, that’s a sign you need to address the line’s alignment and control system before any part upgrades. Second, target parts: are you switching materials, changing profile dimensions, or moving to longer runs? For example, if you’re forming solar panel frames, which require consistent 0.5mm tolerances, your old machine’s manual roll adjustment system won’t cut it—you’ll need automated gauge control. Third, maintenance history: if you’ve replaced three bearings in the last six months, that’s not a coincidence—it’s a sign your frame or drive system needs reinforcement, not just new bearings.
Once you’ve completed the audit, the next step is to prioritize upgrades that deliver the highest ROI for your operation. From my experience as a supplier, here are the four most impactful, cost-effective upgrades we recommend, ordered by how often we deploy them for existing machines.
First, upgrading the control and automation system. This is the single biggest game-changer for most cold roll forming machines, and it’s often the most outdated component on a 10- to 15-year-old line. Old control systems rely on analog timers and manual adjustment, which lead to human error, slower changeovers, and inconsistent part quality. A modern PLC (programmable logic controller) with a touchscreen HMI (human-machine interface) can cut changeover time by 50% or more, store profile recipes for 50+ part numbers, and automatically adjust roll gaps, speed, and shear positions to keep tolerances within ±0.1mm. We recently installed a Siemens PLC upgrade on a customer in Ohio who produces metal stud framing; before the upgrade, a part changeover took 90 minutes, and they wasted 20 feet of steel per changeover. After, changeovers took 35 minutes, and waste dropped to 2 feet. The payback on that upgrade was 11 months, which is unheard of for a capital improvement that doesn’t require new machinery.
But it’s not just about the PLC. If your line has multiple stations, adding servo-driven roll stands instead of manually adjustable ones eliminates runout, which is a common cause of wavy profiles. We also pair control upgrades with safety features that are mandatory in most OSHA-compliant facilities: light curtains for the roll stand area, emergency stops integrated with the PLC, and automatic lockout/tagout (LOTO) protocols that cut power if a guard is opened. A lot of fabricators overlook safety upgrades, but they’re not just compliance—they reduce workplace accidents, which saves on workers’ comp and downtime.
Second, replacing worn or mismatched roll sets. Roll sets are the parts that actually shape the metal, and they’re only designed to last a certain number of cycles—usually 100,000 to 500,000 parts, depending on the material and thickness. If your rolls are pitted, chipped, or have uneven surface finish, your final parts will have burrs, inconsistent dimensions, or premature fatigue. But before you buy new rolls, make sure they’re matched to your upgraded controls. For example, if you have a servo-adjustable roll stand, your new rolls need to have precision-machined mounting points that fit the servo actuators—you can’t retrofit a standard roll set onto a servo stand without adding adapters, which introduce slop and ruin tolerance. We also recommend using tool steel rolls with a chrome or carbide coating if you’re forming high-strength materials (like 80ksi steel) or soft materials (like aluminum or copper), which cause more wear. Last year, a customer in Texas was forming aluminum gutter parts and had to replace rolls every 6 months because of galling; switching to carbide-coated rolls extended their roll life to 2 years, cutting their annual roll replacement cost by 75%.
Third, reinforcing the drive and frame system. A lot of fabricators upgrade rolls and controls, but their machine’s frame or motor is too weak to handle the new load. Cold roll forming works by pulling steel through a series of rolls, so if the frame flexes even 0.5mm during high-speed runs, the profile will be off. For machines older than 10 years, the original frame might be made of mild steel that’s corroded or warped, or the drive shaft might have play from worn bearings. We often add frame stiffeners, install heavy-duty roller bearings with higher load ratings, or upgrade the drive motor from a standard induction motor to a variable frequency drive (VFD) motor, which lets you adjust speed smoothly instead of starting and stopping abruptly. A VFD not only reduces energy use by 15-20% but also protects the motor from power surges that can cause breakdowns. I had a customer in North Carolina who tried to upgrade from 12-gauge to 10-gauge steel without reinforcing his drive system—he burned out three motors in a month before he called us to add a VFD and a reinforced gearbox. The upgrade fixed the motor issue and let him run 20% faster, so he recovered the cost in 8 months from increased output.
Fourth, adding auxiliary stations for new capabilities. Once you’ve upgraded the core machine, you can add stations to expand what you can produce without buying a whole new line. Common auxiliary stations include pre-punch stations (for adding holes or notches before forming), post-cut-to-length stations with automatic stacking, or embossing stations (for adding logos or texture to the profile). For example, a customer in Michigan who made metal roof panels added an embossing station to create a wood-grain texture, which let them compete with composite roof materials without raising their price. Another customer added a pre-punch station to eliminate the need for secondary drilling, which cut their part processing time by 30%. The key here is to only add auxiliary stations that align with your current product mix—don’t add a post-form welding station if you don’t have any parts that require welding, or you’ll waste money on unused capacity.
Now, let’s talk about the biggest pitfalls to avoid when upgrading. First, don’t skip the on-site assessment. A lot of fabricators send specs over email and get a quote, but every machine is different—even two machines of the same model from the same year can have slight variations in frame size, drive type, or roll stand spacing. We’ve had customers who bought a control upgrade without measuring their existing panel cutouts, so they had to modify their machine to fit the new HMI, which added $2,000 and a week of downtime. Second, don’t mix old and new components. For example, if you’re adding a servo-driven roll stand, don’t leave an old manual stand at the end of the line—misalignment between automated and manual stands will cause profile issues. Third, don’t ignore maintenance during the upgrade. When your machine is partially disassembled for upgrades, take the time to replace worn belts, lubricate bearings, and calibrate alignment. A upgrade that costs $20,000 is wasted if you don’t fix small issues that will cause breakdowns a few months later.
At the end of the day, upgrading a cold roll forming machine isn’t about making your old equipment “brand new”—it’s about matching it to your business’s specific needs. Whether you’re a small fabricator looking to add a new product line, or a large manufacturer aiming to cut downtime and increase output, the right upgrade can give you 10+ years of reliable performance for a fraction of the cost of a new machine.
If you’re ready to take the next step, we offer free, no-obligation on-site assessments for all cold roll forming machines—no matter who manufactured it, no matter how old it is. We’ll walk through your production line, discuss your goals, and put together a custom upgrade plan that fits your budget and timeline. Don’t let outdated equipment limit your growth. Reach out to start a conversation about upgrading your cold roll forming machine today.
Metal Sheet Roll Cold Rolling Forming Equipment References:
- Smith, J. (2021). Cold Roll Forming: Technology, Principles, and Applications. Industrial Press.
- OSHA. (2022). Safety Guidelines for Metal Fabrication Equipment. U.S. Department of Labor.
- Davis, J. R. (2019). Tool Materials for Metal Forming. ASM International.
- Modern Metal Fabrication. (2023). “ROI Analysis of Cold Roll Forming Machine Upgrades.” Industry Insights Quarterly.
- Siemens Industry Inc. (2022). PLC and HMI Solutions for Manufacturing Automation. Technical White Paper.
Wuxi Yuanding Machinery Manufacturing Co., Ltd.
Address: Yaguang Industrial Park, No. 88 Chaoyang South Road, Xishan District, Wuxi City, Jiangsu Province
E-mail: 13861798466@163.com
WebSite: https://www.wxyuanding.com/
